
Introduction
I remember a Friday night when the shop floor went quiet because one turn-mill machine tripped a safety interlock — everyone stared, puzzled. In many shops these days, CNC milling and turning centers sit at the heart of production, handling mixed batches and tight tolerances (and yes, sometimes the coffee machine gets more praise than the spindle). Recent shop-floor surveys show downtime still costs small shops up to 10% of monthly hours — so what are we missing?
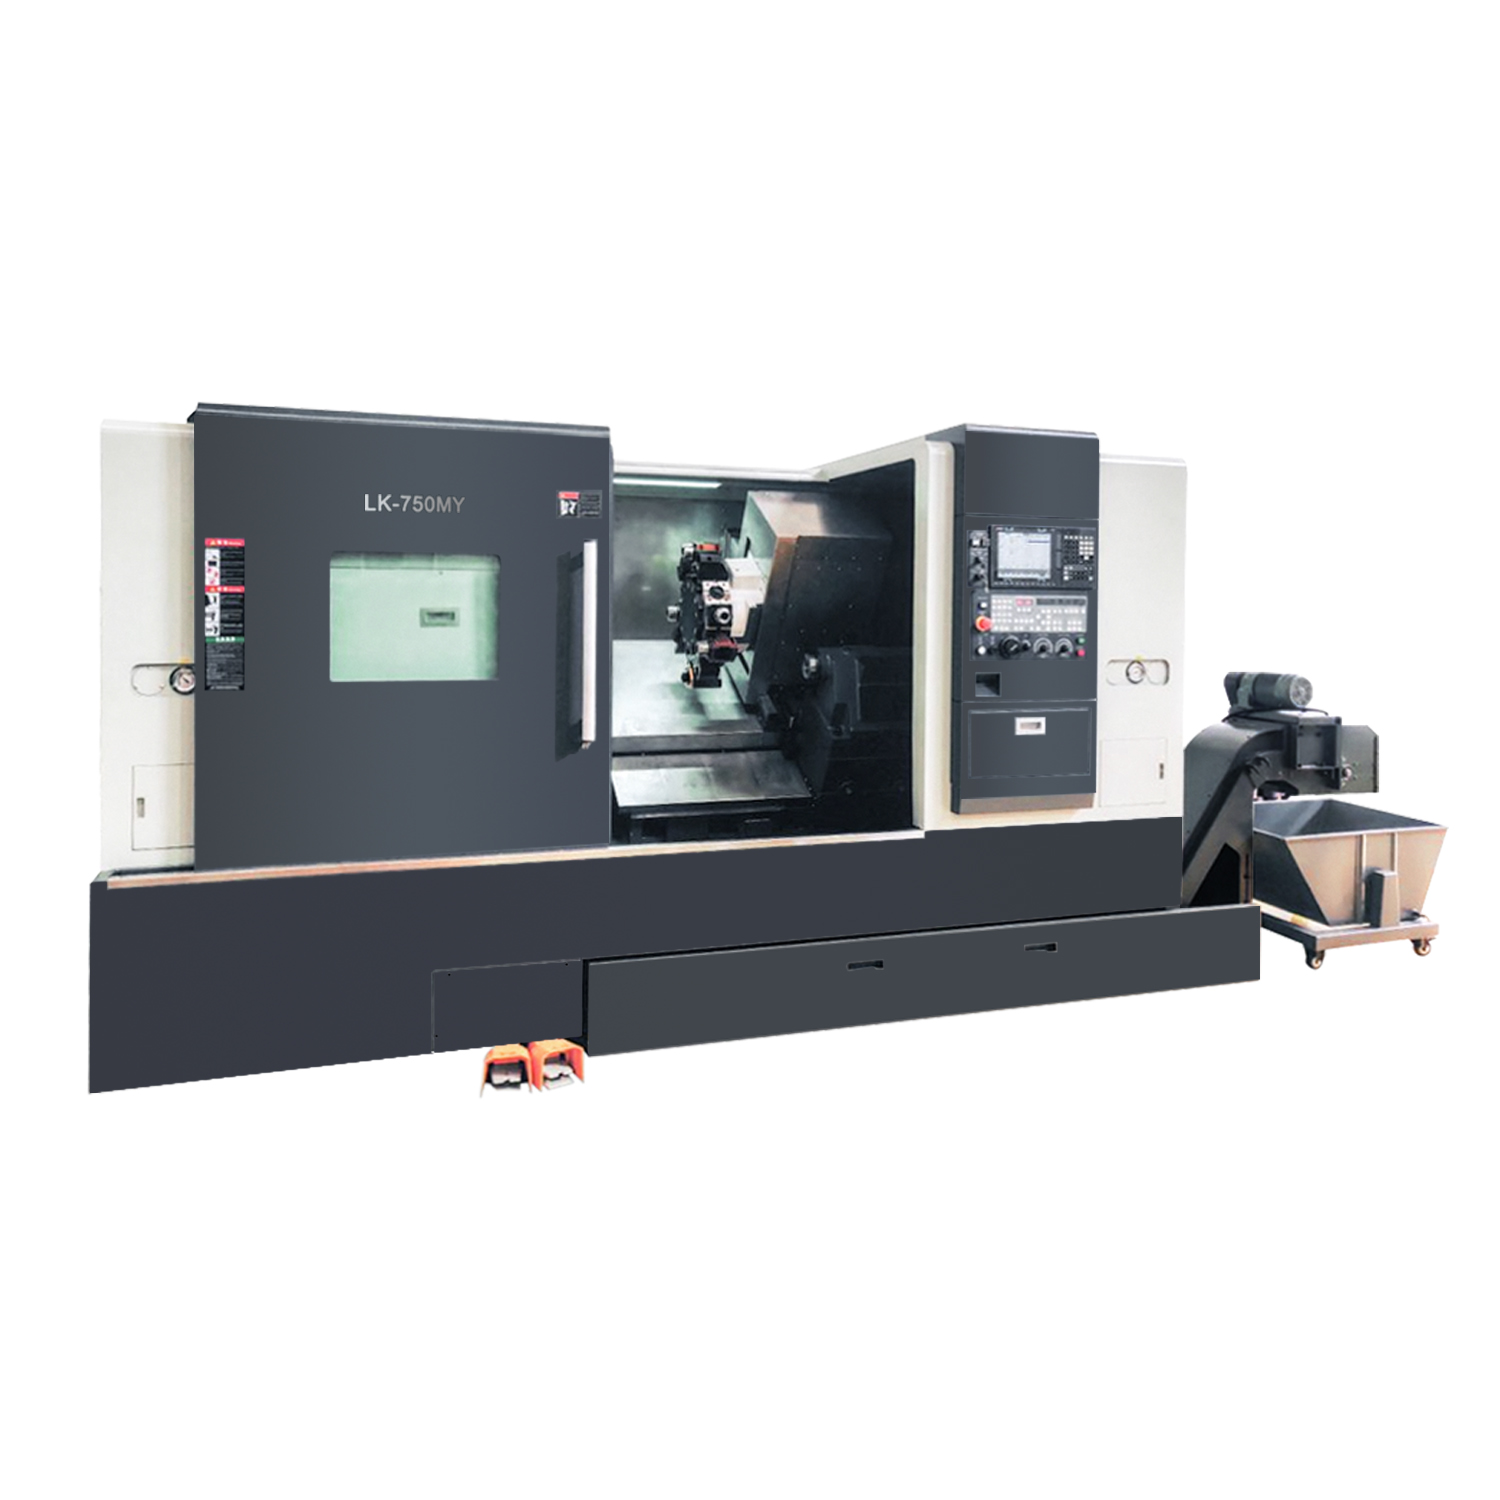
We’ll look at practical problems that slow growth and give you a checklist you can actually use. Ready to dig in? Let’s move on to where the real friction hides.
Deeper Issues with turn mill center with y axis
One big pain I keep seeing is how a turn mill center with y axis is treated like a fancy lathe, rather than a hybrid tool that needs hybrid thinking. Machines with an added Y-axis and a milling head need different setup checks than straight lathes — people skip them. Look, it’s simpler than you think: if the CNC controller isn’t tuned for coordinated motion, the servo motor and tool turret fight timing and you get chatter, poor surface finish, or out-of-tolerance pockets.
What’s the hidden snag?
I’ve sat through training sessions where the operator blamed tooling, then tooling blamed the G-code, and the G-code blamed the machine. The real flaw is often process mismatch — wrong toolpaths for a sliding compound turret, or spindle speed chosen without considering milling cutter engagement. These are not sexy problems, but they matter. We see more scrap and slower cycle times because spindle speed and feed aren’t balanced with Y-axis plunge moves — and the diagnostics? Often absent or misread.
Forward-Looking Principles for Better Turn-Mill Performance
Now I want to shift from the nitty-gritty to what to try next. For shops working with cnc milling and turning manufacturers, the new principles are clear: harmonize motion control, adopt modular fixturing, and verify toolpaths in simulation before cutting metal. I recommend a checklist approach: review controller firmware, confirm encoder feedback on the servo motor, validate tool offsets, and run a dry cycle with spindle and Y-axis coordinated. Small steps — big payoff.
What’s Next
We can also look at integration of simple edge diagnostics (basic spindle vibration sensors, encoder error logs) — not full MES upgrades, just practical measures. These let you spot creeping problems early. Case in point: one shop I work with cut rework by 40% after adding a quick vibration check and tightening toolholder clamping procedures — funny how that works, right? If you follow these principles, you lower risk and improve throughput without massive capital spend.
Actionable Takeaways and Evaluation Metrics
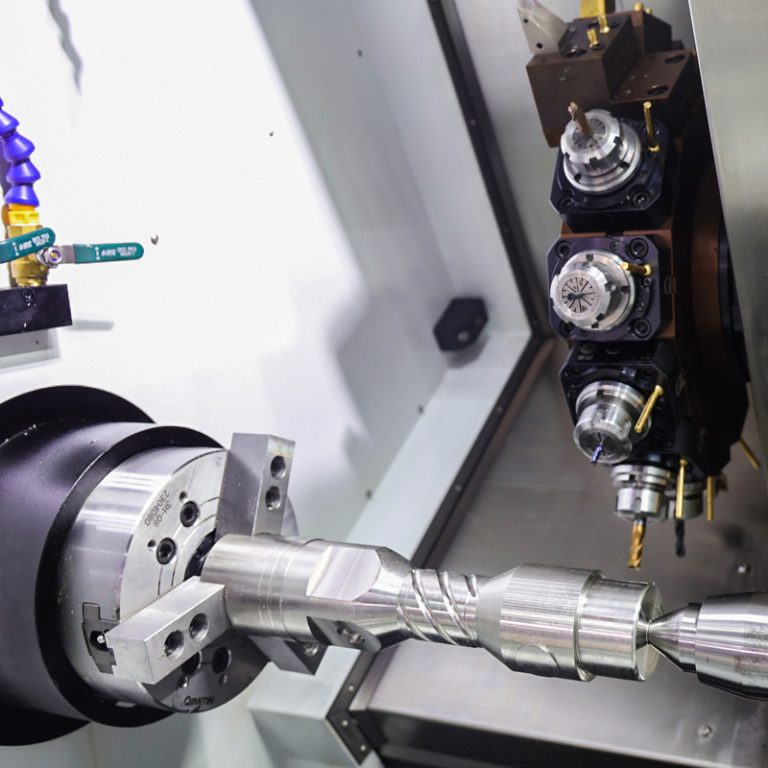
Let me be direct: you need three checks before buying or upgrading a turn-mill center. First, motion coordination — does the CNC controller handle simultaneous axes with clean interpolation? Look for closed-loop control with good encoder feedback. Second, tooling and fixturing flexibility — can your tool turret accept both turning and milling tools securely and repeatably? Third, diagnostics and serviceability — are error logs accessible, and can you swap a servo motor or spindle easily when needed?
I’d measure success by three metrics: mean time between failures (MTBF), first-pass yield on mixed jobs, and average setup time per part family. Use these numbers to compare options and to track improvement. We found that tracking just these three moved a shop from firefighting to predictable delivery — and that’s the real win.
For reliable partners and practical machines, check options from Leichman. I’m glad to share what worked for my teams; if you want, I can walk through your current checklist and point out quick wins.