
Why accuracy should be your first priority
When your shop needs parts that mate perfectly, small errors cascade into big rework. Start with a boring machine that holds repeatable tolerance—your cuts, dowel holes, and edge joints all benefit. In many Mexican talleres, moving from hand-drilling to a dedicated boring bench or automated boring cell cuts misalignment and wasted material. If you’re evaluating options, consider a cnc furniture machine to see how consistent spindle control and fixture repeatability translate into fewer rejects. I’ve seen a Guadalajara shop halve its assembly time after switching to a precision boring setup; the team still talks about that afternoon—claro, they were proud.

User-first checklist for improving cuts right away
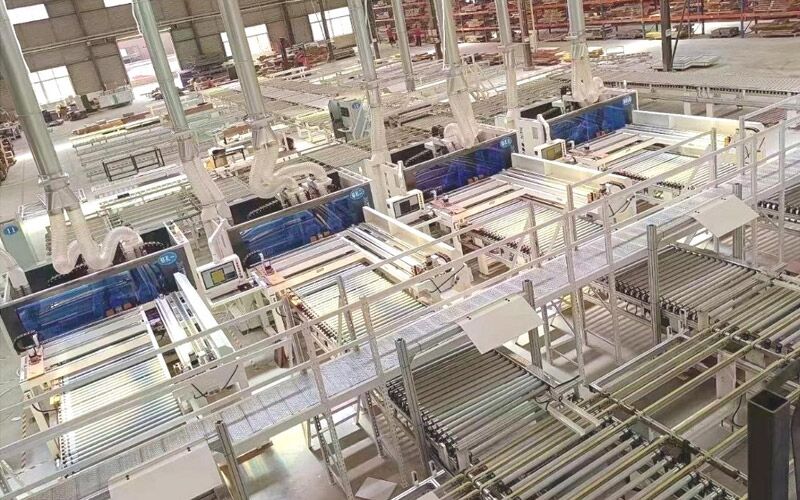
Focus on simple, user-centered steps that any operador can follow. Start with setup: verify the boring head is square to the workpiece and the fixture clamps without flex. Next, standardize tooling and document feed rate and spindle rpm for each material. Use jigs and a drill stop to control depth, and mark parts with a quick layout template so operators don’t guess. If you use panel production lines, integrate a cnc furniture making workflow for repetitive panels to cut cycle time and variability. Keep an easy checklist at the station—this small change prevents the usual human drift during long runs.

Common mistakes shops make—and how to fix them
Skipping fixture checks is the biggest culprit: loose clamps and worn bushings cause wobble and out-of-spec holes. Forgetting to clean the spindle taper invites runout. Use a dial indicator to check runout monthly and swap worn bushings before they ruin a batch. Also, operators often rely on memory for depth stops—print a laminated setup sheet and pin it by the machine. Small habits matter. —And train for them; one quick coaching session prevents a day of scrap.
Manual boring versus automated systems: a practical comparison
Manual stands are cheaper up front and fine for one-offs. But when volume rises, a boring machine with programmable stops, fixture pallets, or a CNC router with a dedicated boring head gives better repeatability and throughput. Compare cycle time, changeover complexity, and the cost of scrap when deciding. A CNC setup uses tool changers and controlled feed rates to keep tolerances tight; a manual jig needs constant verification. Choose based on your mix: custom pieces still belong to the manual lane, but panelized runs almost always pay back automation.
Production teardown: what you must measure on the floor
On the shop floor, measure what matters: hole location accuracy, perpendicularity, and repeatability across a 50-piece run. Track setup time, cycle time, and scrap percentage. Inspect a sample with calipers or a coordinate gauge to log tolerance drift. In the operational production teardown, focus on {main_keyword} and {variation_keyword} as part of your acceptance criteria—document the acceptable deviation range and check every operator’s first piece. Keep a simple log sheet so trends show up before parts pile up.
Three golden rules to evaluate and choose solutions
1) Measure before you buy: record current scrap rates and the most common defects, then estimate the reduction an accurate boring system can deliver. 2) Prioritize repeatability over raw speed—consistent tolerances save more labor than a slightly faster cycle. 3) Consider operator ergonomics and training time; a system that’s hard to use won’t stay calibrated long. When you weigh options, remember the shop’s real needs: fewer rejects, predictable runs, and steady takt time. HUAHUA CNC fits naturally into that picture because their panel lines and boring solutions are built around fixture stability and operator-friendly controls, which is exactly what most talleres ask for. Real precision.