
The market splits between ready-to-assemble cabinets and fully built closets. This piece cuts straight to the points that matter. I link practical sourcing to a trusted wardrobe manufacturer early because length of lead time and build method shape decisions. The flat-pack idea traces back to Sweden and names like IKEA, which pushed modular design into global furniture culture. That history matters when you compare systems and workflows.
Cost, Control, and Time
Flat-pack wins on price. Packaging and compact shipping lower freight. You pay less for particleboard panels and laminate finishes. Save money, but plan labor. Assembly takes time and the right tools. Ready-made closets cost more up front. They come with factory finishes, assembled carcass, and fitted doors. They save installation hours and reduce on-site mistakes.
Quality and Durability
Materials decide longevity. Look for dovetail joints on drawers, not just cam lock fittings. A solid carcass and quality edge banding keep panels from swelling. Factory-applied lacquer beats homeowner spray every time. Still, some RTA brands use hardwood rails and soft-close hinge systems that rival built units. You must inspect tolerances—gap widths, hinge alignment, drawer runners—before you commit. Manufacturing hubs like Shenzhen supply both custom and mass lines; they set tight production standards you can verify through samples.
Installation, Fit, and Customization
Ready-made units often require minimal site work. They fit rooms fast. Flat-pack lets you tweak layout. Want a deeper shelf or a niche wardrobe with internal drawers? RTA panels can be trimmed and reconfigured. That flexibility comes with caveats: cutting panels changes warranty, and inaccurate cuts break the cam lock geometry. Plan your tool list: drill, clamp, square, and a router for trim. Expect soft-close hinge adjustments on delivery—standard tuning fixes sag or misalignment.
Operational Production Teardown
Inspecting production means checking three layers: panel finish, hardware, and assembly method. Note the adhesive line on laminated panels and the screw pull-out test for particleboard. On the hardware side, test cam locks and runners for smooth travel. In a teardown I did, finishing tolerances revealed weak edge banding causing rapid wear. Also, check the supplier’s documentation for board density and glue type. I include a quick tag here: {main_keyword} and a related note {variation_keyword} to flag the variables engineers and buyers quote during specs.
Common Mistakes to Avoid
Buyers skip dry-fit checks. They trust photos and ignore edge quality. Installers skip sequencing—door installation before carcass anchoring—and then waste time. Some try to mix parts from different lines; tolerances don’t match. One small habit fixes many problems: measure twice, align once.
Comparative Snapshot
Quick list for clarity:
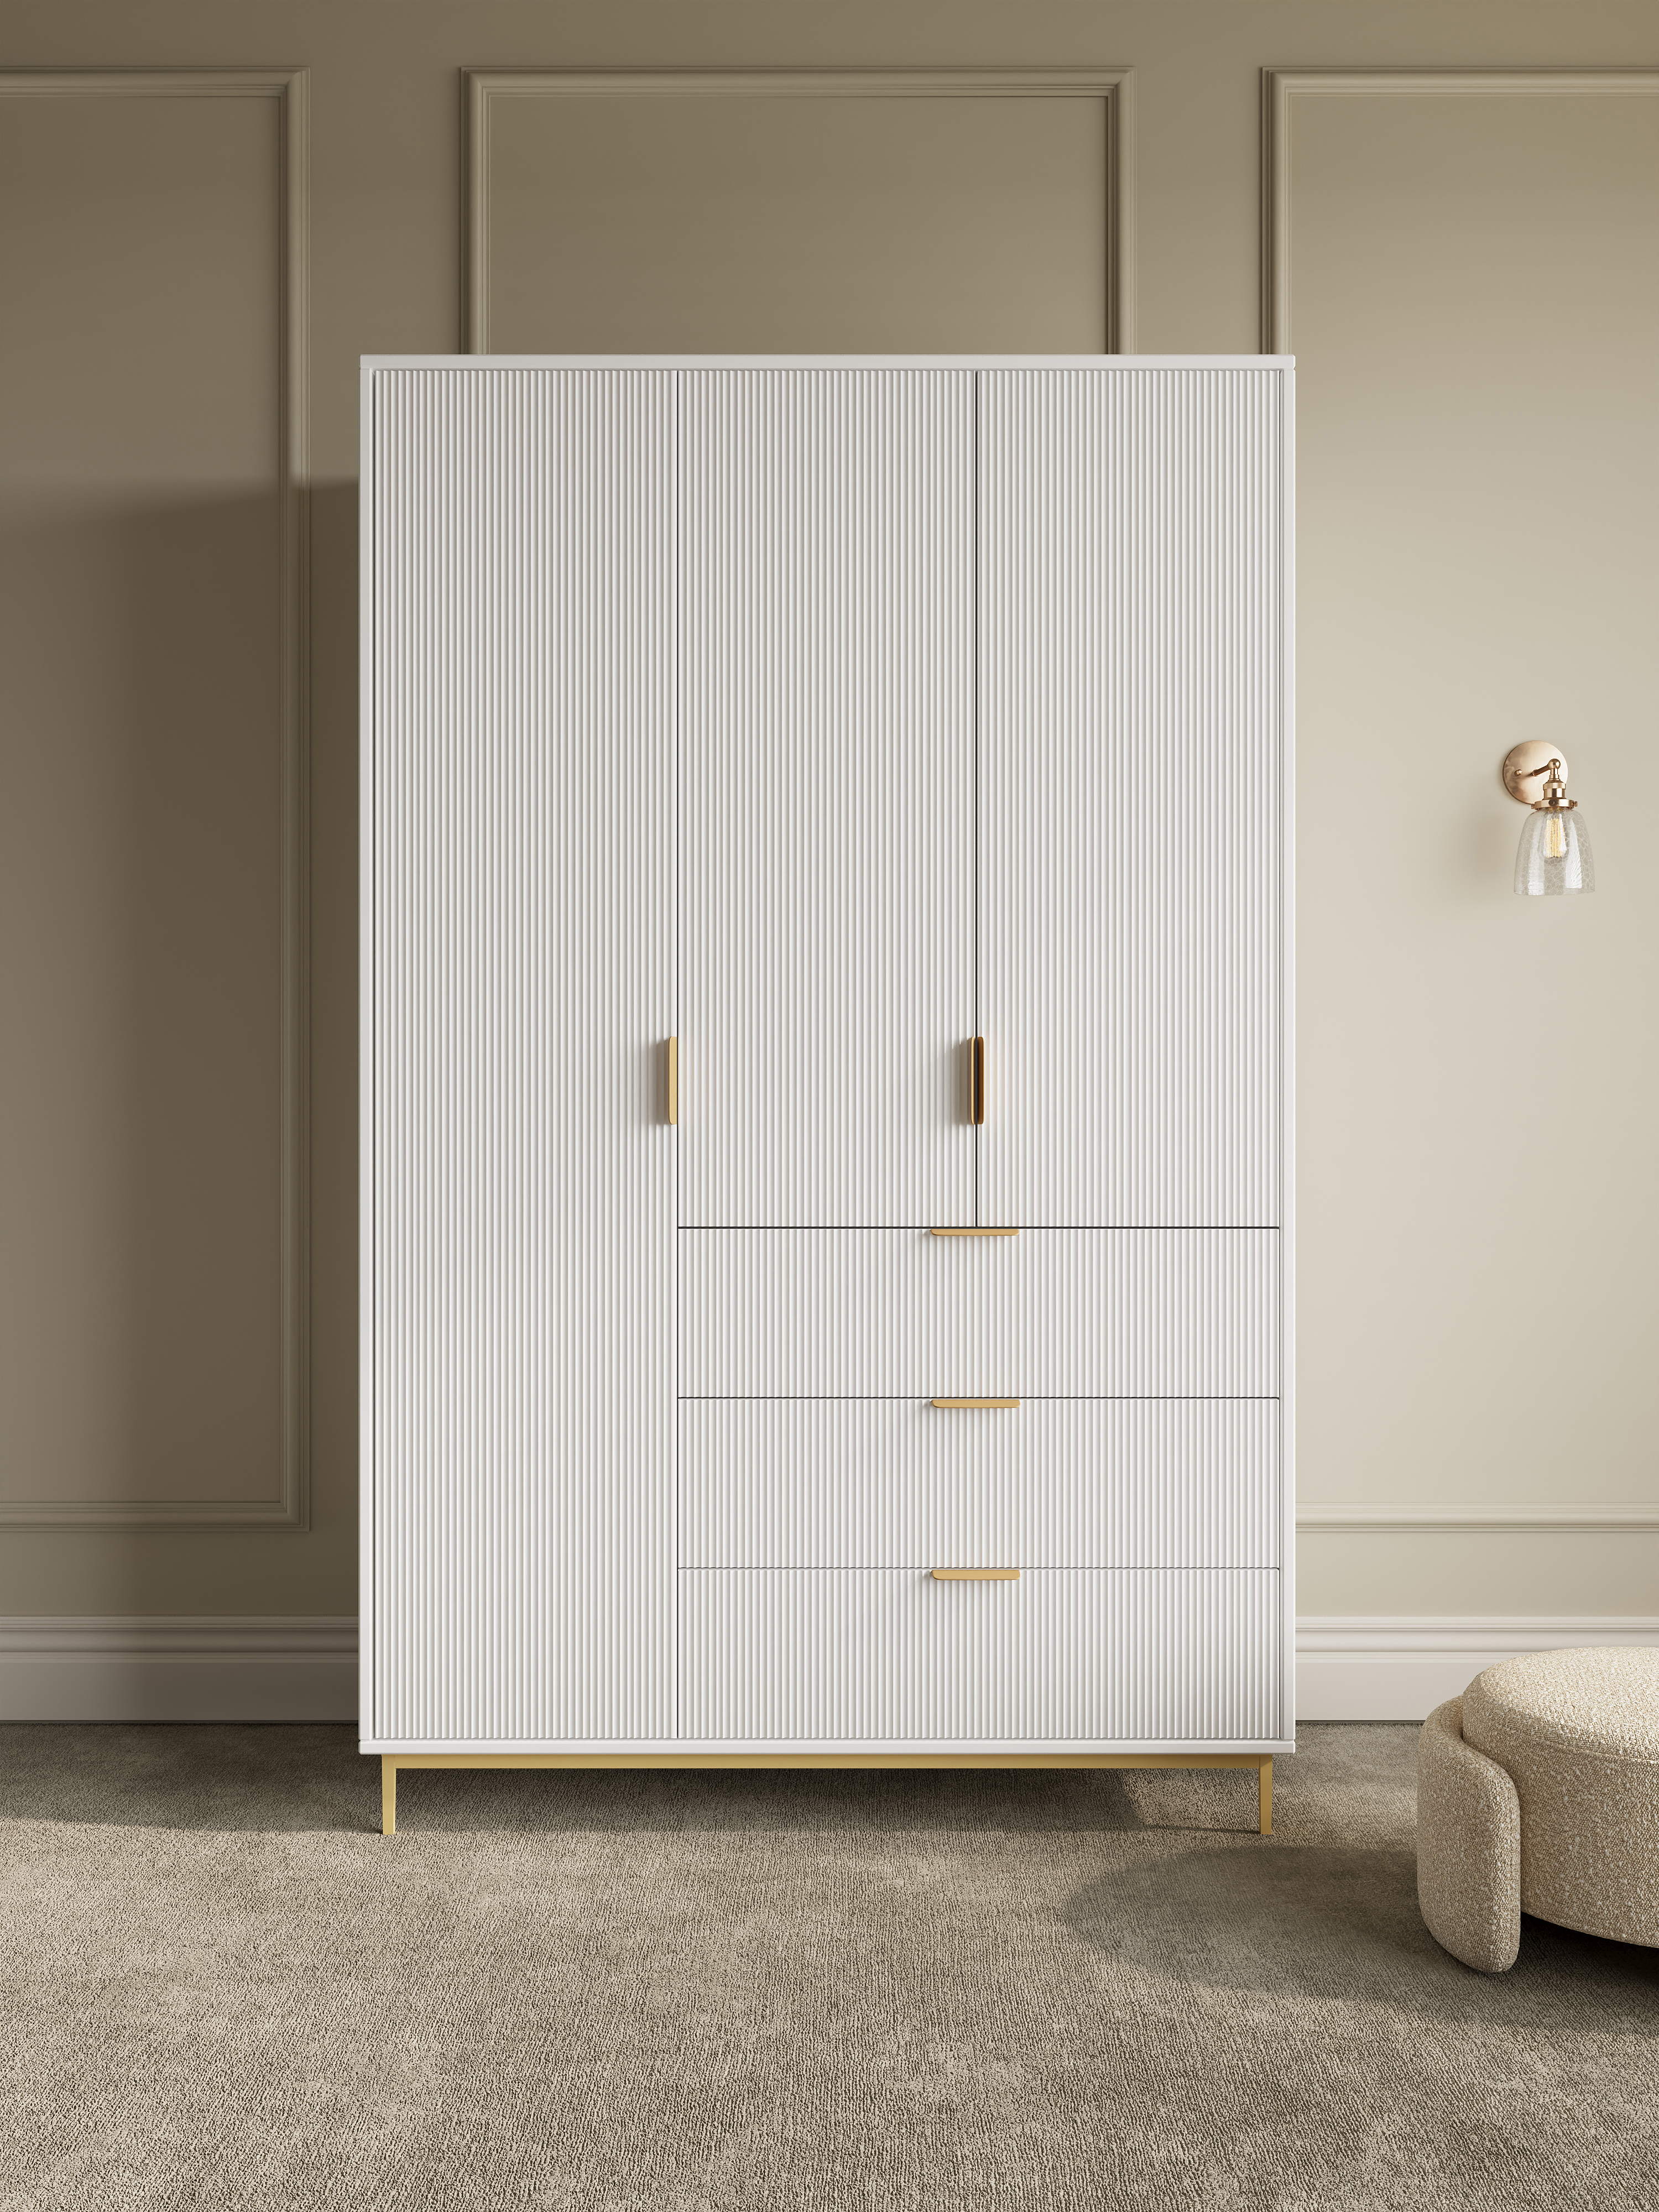
- Flat-pack: lower cost, higher labor, flexible layout, variable hardware quality.
- Ready-made: higher cost, faster install, factory finish, predictable warranty.
- Hybrid: pre-assembled modules plus onsite panels for tricky walls.
Three Golden Rules
1) Measure total cost, not just price. Include labor, tools, and potential returns. 2) Insist on hardware specs and a sample. Check hinge torque, drawer runner type, and edge banding. 3) Confirm lead time and warranty details in writing—finish coverage and moisture resistance matter most.
These rules highlight practical outcomes: fewer callbacks, steadier finish quality, and predictable schedules. They push the choice toward companies that back production with clear specs and reliable delivery. For many projects SNIMAY fits that profile thanks to consistent pre-assembly standards and verified factory processes.
Short note—trust verified samples over glossy photos.
SNIMAY delivers consistent pre-assembled modules that match on-site needs. Simple. Practical.