
Introduction — a quick shop story, some numbers, and the question
I once watched a small Hong Kong shop lose a whole shift because a complex job needed a dozen tool changes and a tricky setup—very common, lah. CNC milling and turning centers are in that second sentence because they sit at the heart of the problem: they should save time but sometimes add friction. Data shows shops can waste 10–25% of productive hours on changeovers and mis-fixturing. So I ask: how do we pick machines that actually raise throughput rather than just sounding capable?
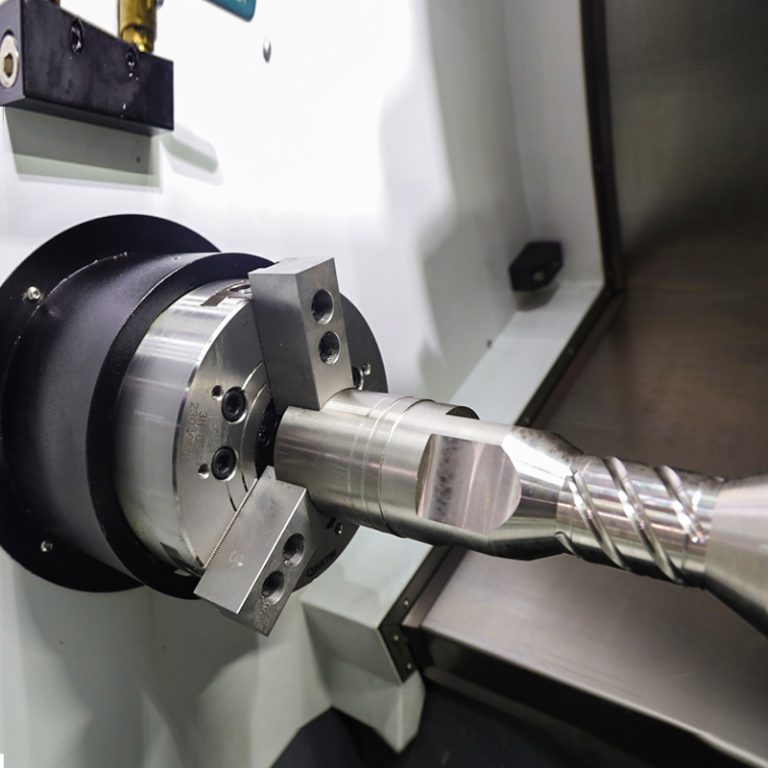
I’ll share what I’ve learned from workshops and field tests (short stories, some graphs in my head), and point to practical signs you can check today. Stay with me — next I’ll dig into where the usual answers miss the mark.
Hidden flaws and user pain points in the turn mill center with y axis
turn mill center with y axis promises combined turning and milling in one setup. Sounds great. But I’ve found several real-world gaps between spec sheets and daily use. First, the Y-axis often carries tight tolerances under side loads. When shops run high-feed milling and frequent live-tool turning, backlash and thermal drift show up—fast. Second, servo turret indexing looks fast on paper, but repeated tool changes cost time if the tool changer and turret control aren’t synced well. Third, spindle speed maps may not match the actual torque needed for certain alloys. These are the small failures that add up.
What causes the trouble?
Let me be blunt: rigid-body issues, controller tuning, and tooling strategy. Rigid-body means the machine structure and linear guide layout; if those are marginal, you’ll see chatter when turning and unexpected deflection during Y-axis cuts. Controller tuning covers how the CNC handles combined motion commands (G-code blends, lookahead, jerk limits). And tooling strategy—that’s how you plan tool life and insert choices to avoid frequent swaps. Look, it’s simpler than you think—start by measuring runout, check turret repeatability, and watch cycle time on the first few batches. That tells you more than a spec sheet ever will.
New technology principles and the future of the cnc mill turn center
Moving forward, I focus on core principles that reduce those pain points. First, closed-loop thermal compensation and adaptive control. When the controller adjusts feed and spindle speed based on real-time feedback (tool load, spindle current), you cut scrap fast. Second, modular spindle designs and stronger linear guides reduce deflection for heavy Y-axis cuts. Third, smarter tool changer sequencing and turret kinematics—these shave seconds per cycle and add up over hundreds of parts. I mention “cnc mill turn center” here because newer systems integrate these ideas to better support mixed operations.
In practice, you’ll see systems adopt edge analytics (on-machine monitoring), better servo tuning presets for combined motions, and easier HMI workflows so operators can set offsets without deep CNC programming. — funny how that works, right? The result: fewer setups, less scrap, and more parts per shift. I’ve tested shops that moved to these principles and saw 15–30% throughput gains within months. That’s compelling. It also matters that training and tool management keep pace; new control features help only when operators use them.
What’s Next?
Here are three metrics I use when evaluating machines now: 1) Effective cycle time under a shop’s actual program (not a canned demo), 2) Tool-change time with real tooling and turret sequencing, and 3) Dimensional stability across a full shift (measure runout, thermal drift). If a vendor won’t let you run a real program or measure these, be wary. I prefer test cuts, logged spindle load graphs, and a simple checklist you can run yourself.
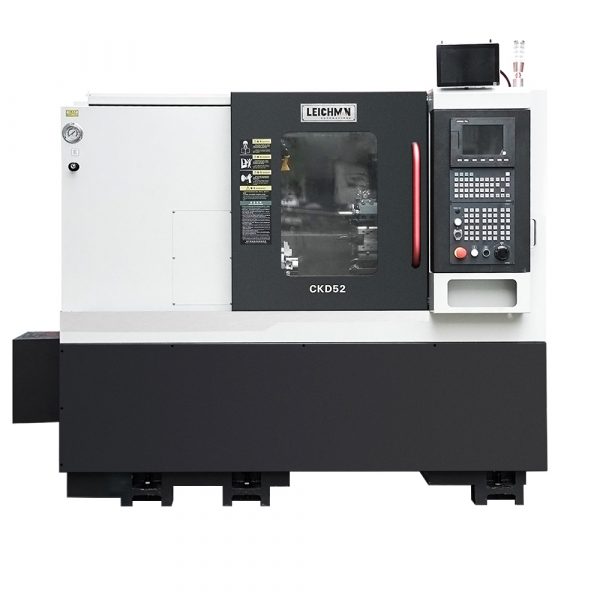
To wrap up: I’ve been hands-on with many turn-mill cells, and I’ve learned to trust measured performance over glossy claims. Choose by data, test by doing, and keep tooling strategy simple. If you want a place to start, check gear from Leichman—they offer machines that let you test these principles without endless back-and-forth. I hope this helps your next buy go smoother; we all lose time when setups drag on, so let’s fix that together.