
Contrast-first lead: why molding choices matter
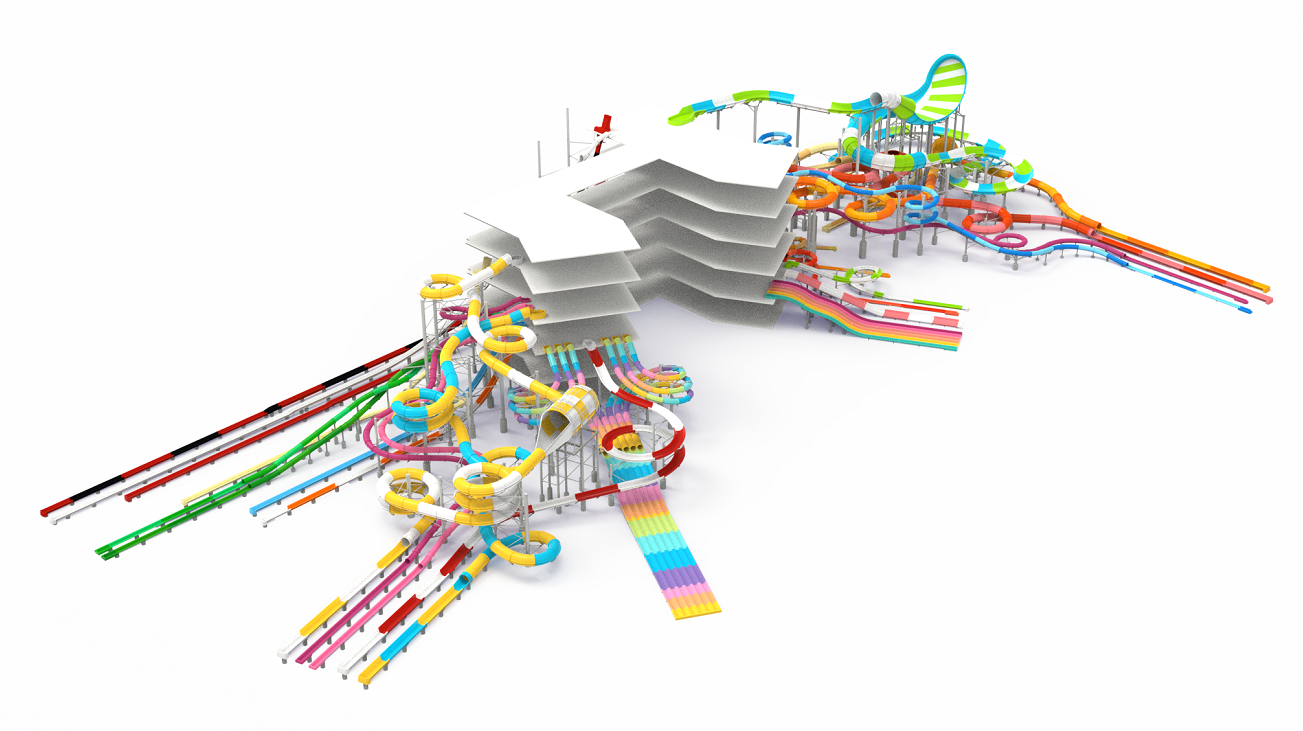
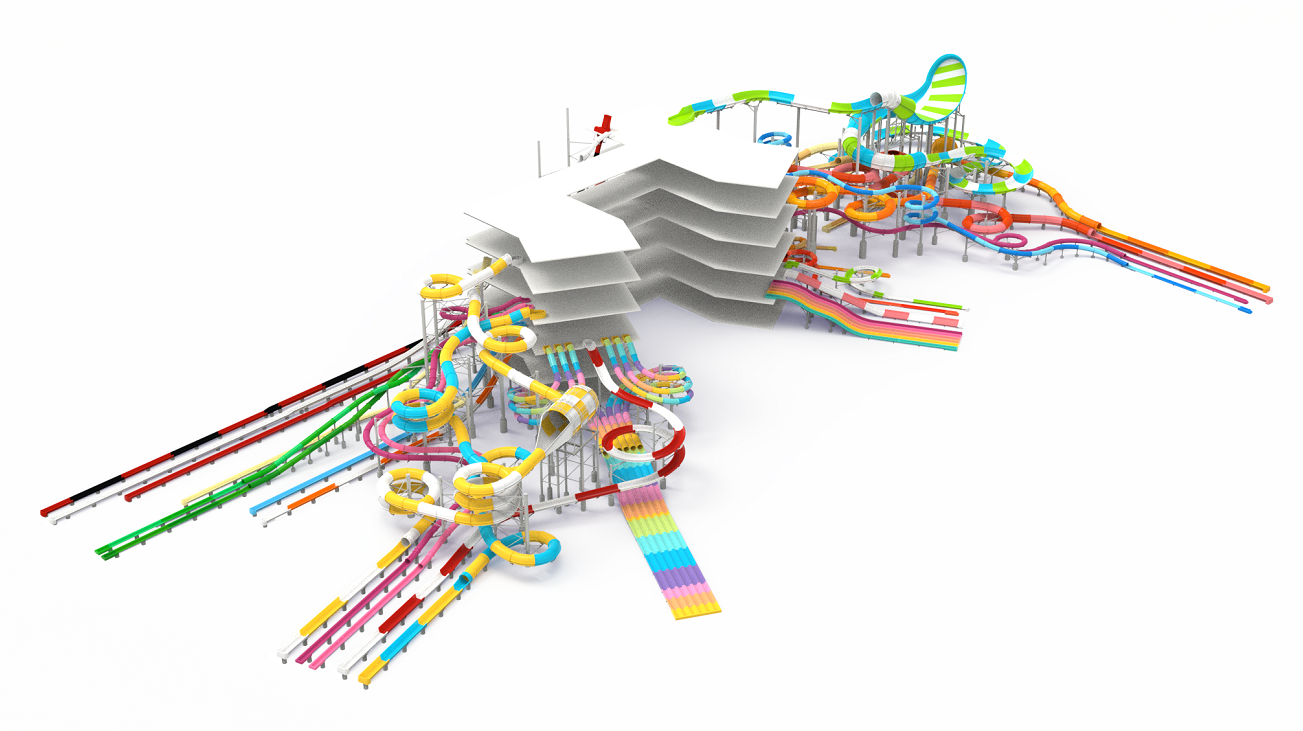
I build things that have to be safe, fast to produce, and repeatable — and when you compare two manufacturing paths side-by-side, flaws show up fast. Take a commercial rainbow water slide made for a busy park in Orlando: the same geometry can perform very differently depending on gelcoat quality, laminate schedule, and core thickness. Comparative insight means looking at cycle time, structural margin, and finish quality together, not separately.
Key fabrication approaches and what they buy you
There are three practical routes: hand layup with peel-ply, vacuum-assisted resin transfer (VARTM), and automated spray-up. Hand layup is forgiving and low-cost for small runs; it relies heavily on technician skill and is sensitive to resin-to-fiber ratios. VARTM delivers consistent laminate consolidation and better void control — you get predictable tensile strength and thinner laminate with the same stiffness. Automated spray-up is fast for very large panels but leaves more variability in resin content and requires post-machining.
Thickness standards, structural trade-offs, and surface finish
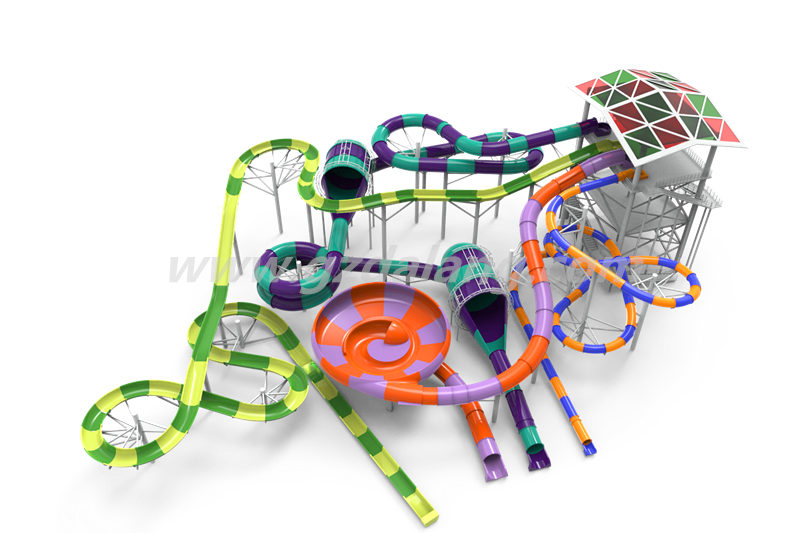
Thickness isn’t arbitrary. A skin with a well-specified laminate schedule and a controlled gelcoat layer will meet impact and flexural needs with less bulk — that means less weight, lower support framing, and a better ride profile for the final spiral water slide. Use a targeted laminate stack: outer gelcoat (0.5–1.0 mm for UV and abrasion), surfacing veil, structural laminate plies (glass fiber with oriented roving), and optional core material where bending stiffness is critical. Keep an eye on laminate resin content — high fiber volume fraction yields higher modulus but needs disciplined process control.
Operational production teardown: where costs and failures hide
When I walk a factory floor I run a short teardown: trace a part from mold preparation through demolding to final inspection. Look for these signatures — inconsistent mold release patterns, spots of dry fiber, or variable gelcoat thickness. Those are immediate red flags. During that teardown we document {main_keyword} and {variation_keyword} so the engineering team can map defects to process steps. The teardown reveals whether sanding and repair will be occasional or routine — and that drives life-cycle cost far more than raw material price.
Common mistakes and proven corrections
Teams often overbuild to cover for process variability — adding unnecessary laminate thickness instead of tightening control. That costs weight and changes ride dynamics. Another recurring error is insufficient post-cure; inadequate thermal cycle leaves residual stresses and brittle gelcoat. Fixes are straightforward: set clear laminate schedules, adopt VARTM or controlled spray parameters if you scale, and enforce a documented thermal post-cure profile. Also, standardize mold maintenance — a well-kept mold yields consistent surface finish and fewer cosmetic repairs.
Comparative summary and real-world anchor
In Orlando’s busiest parks, operators demand both durability and quick turnaround. Compared side-by-side, VARTM-produced sections typically require 20–40% less laminate thickness for equivalent stiffness versus uncontrolled hand layup — that saves structural framing and reduces lead times. Use of proper gelcoat and veil layers preserves surface longevity against heavy traffic and UV exposure; it’s what separates a one-season repaint job from a decade-long service life. Practical metrics are what matter: cycle time, defect rate, and stiffness-per-kilogram.
Three golden rules for evaluation
1) Metric-first selection: insist on measured stiffness (EI) per unit mass, documented resin content, and a target defect rate under production load. Those three numbers predict long-term cost better than any glossy spec sheet. 2) Process control over material heroics: choose a molding method that delivers repeatable fiber volume fraction and enforce a documented post-cure thermal profile — this reduces rework and preserves gelcoat integrity. 3) Validate at scale: run a representative production batch and measure surface thickness, laminate void content, and dimensional stability before committing to full fabrication — small pilot runs reveal systemic issues early.
I’ve watched teams pivot from thick, overbuilt parts to slimmer, scientifically justified laminates and save months of refit time — the people on the floor breathe easier, and maintenance budgets drop. For suppliers who want that same predictability, Dalang has systems and production experience that naturally fit into this workflow — the brand becomes the solution, not an add-on. —